An order of 300 pendants arrived with a white residue along the bail on roughly one piece in eight. The residue was polishing compound left in a recess that the final rinse did not reach. The retailer spent two days cleaning stock before it could be photographed for the site.
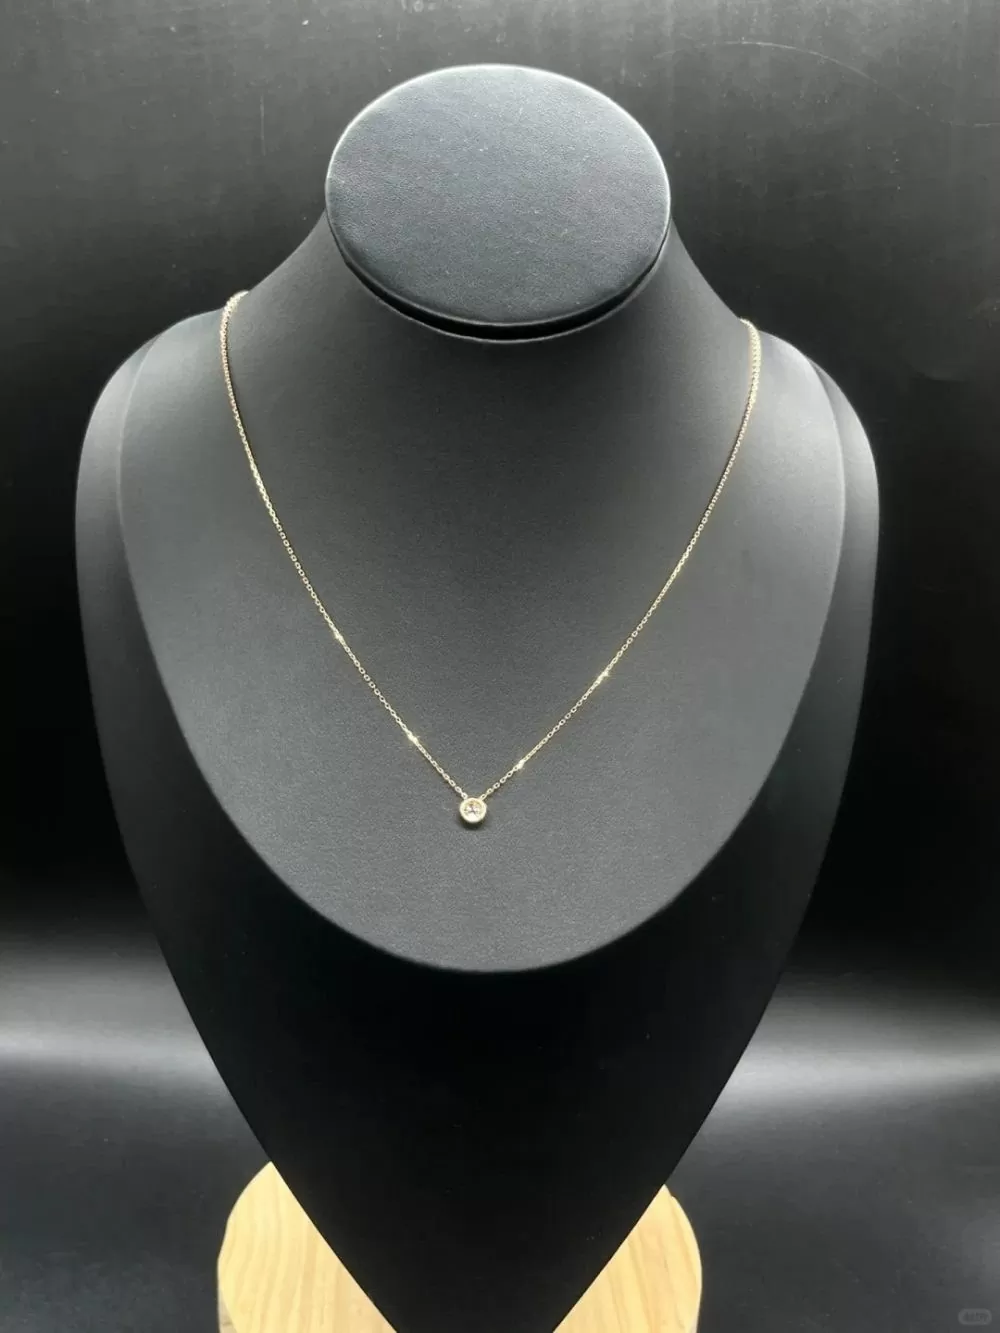
Final inspection is the last cheap moment to catch a defect. Once the box closes, every defect costs freight, labour and a customer conversation, and the cost is multiplied by the number of pieces in the shipment.
Why final inspection catches what in-process checks miss
In-process checks happen while the piece is apart. Final inspection happens when it is assembled, plated and packed, which is the state the customer will see.
The assembly effect
Setting a stone can shift a prong, and plating can cover a scratch that appears as a shadow. A piece that passed a bench check before plating can fail after it, and only a post-plating check sees that.
The residue effect
Polishing compound, plating solution and ultrasonic residue all hide in recesses until the piece is dry. A dry, assembled piece is the only reliable subject for a residue check.
The seven checks
Seven checks, performed in order, cover the defects that cause most wholesale returns. The order matters because each check assumes the previous one passed.
| Step | Check | Defect caught |
|---|---|---|
| 1 | Residue and cleanliness | Compound in recesses, fingerprints |
| 2 | Plating colour and thickness | Patchy plate, wrong tone |
| 3 | Stone seating | Loose stone, uneven girdle |
| 4 | Prong integrity | Short prong, cracked tip |
| 5 | Surface finish | Scratches, tool marks |
| 6 | Function | Clasp, hinge, chain stretch |
| 7 | Paperwork match | Wrong certificate or tag |
Each step is a few seconds per piece. The whole routine runs under two minutes on a simple pendant and about four on a stone-set ring.
Step one: residue and cleanliness
Inspect under a daylight lamp at an angle, not straight on. Residue shows as a faint white or grey line in a recess when the light rakes across it. Straight-on light hides it, which is why pieces with residue reach customers.
Pay particular attention to the bail, the gallery under the stone, the inside of a clasp and any milgrain detail. These are the four places where cleaning fails.
Step two: plating colour and thickness
Compare the piece against a reference piece plated in the same batch. Colour drift between pieces in one order is a bath problem, and it is easier to see against a reference than from memory.
Check the high points first. A patchy plate shows at an edge before it shows on a face, because the current density at an edge differs from the centre.
Step three: stone seating
Touch each stone with a soft probe, never a metal tool. A stone that moves is unseated, and a stone that moves after plating was likely loose before it. Look along the girdle line for a stone sitting proud or sunk.
Step four: prong integrity
Check that every prong tip sits on the crown of the stone and that none is short. A short prong passes a casual look and fails in wear, and it is the most common cause of a lost stone claim.
Step five: surface finish
Rotate the piece under the lamp and look for scratches that run in one direction. A directional scratch is a tool mark from finishing, not from shipping, and it will read as a defect to a customer.
Step six: function
Open and close every clasp, hinge and earring post. A clasp that sticks on the first open will stick for the customer, and a chain that has stretched during setting will not hang correctly on a bust.
Step seven: paperwork match
Match the certificate number, the tag and the packing list line to the piece in hand. A mismatched certificate is a compliance problem, not a cosmetic one, and it is the defect that is hardest to fix after shipping.
Sampling for bulk orders
Inspecting every piece is feasible under 100 units. Above that, sampling is the practical route, and the sampling method decides whether it works.
Rotate the sample
Sampling the same position in every box means the same pieces are never checked. Rotate the sample across positions so that every position is inspected at some point in the run.
Escalate on a failure
A failure in a sample triggers a full inspection of that box, not a note in a log. A single failed piece in a sample of fifty usually means several in the box, and the pattern matters more than the count.
Recording the inspection
A record turns a routine into evidence. Three fields make it useful.
- Order number, date, inspector name
- Pieces checked, pieces failed, defect type per failure
- Action taken: rework, replace or accept with note
Over a few months this record shows which defect dominates. A programme with recurring prong failures has a setting problem; one with recurring residue has a cleaning problem. Neither is visible without the record.
Cleaning methods and when to use them
The cleaning method has to match the piece. A method that is safe for a diamond solitaire can damage a coated stone or thin plating.
| Method | Suitable for | Avoid on |
|---|---|---|
| Ultrasonic | Solid metal, durable stones | Coated stones, pearl, opal, glued settings |
| Steam | Solid metal, well-set stones | Coated stones, porous stones |
| Soft brush and soap | Everything, including coated | Nothing, if the brush is soft |
| Chemical dip | Heavy tarnish on unplated silver | Plated pieces, treated stones |
For a mixed order, the safest default is a soft brush with mild solution and a thorough rinse, followed by a warm air dry. It is slower than ultrasonic and it does not damage anything.
Freight damage versus factory defect
The first question on any claim is where the defect happened. The answer decides who pays, and it is usually visible in the photographs.
Defect signatures
A factory defect is consistent across pieces: the same prong short on every ring, the same patch of thin plate on every pendant. Freight damage is scattered: one bent prong, one scratched face, one broken chain on a single piece.
Photograph before unpacking
Photograph the sealed box, then the packing layer, then the pieces as they sit. A claim supported by three photographs taken before handling is far stronger than one supported by a photograph of the piece after it has been picked up.
The claim window
Agree the window in writing, typically seven days from delivery. A window that runs from dispatch rather than delivery gives the buyer no time to inspect, and a window with no stated length gives neither side a reference.
Name the recipient as well. A window that starts when the courier hands over the parcel is workable, and a window that depends on the buyer's warehouse receiving process should be written to match that process rather than left to interpretation.
Packing after inspection
Packing is the step where an inspected piece becomes uninspected again. Three practices protect the result.
- Handle with gloves after the final polish
- Wrap each piece individually before it enters a box
- Do not stack pieces that can contact each other
A piece that passes inspection and then sits loose in a box with forty others will arrive with scratches. The inspection was correct and the packing undid it.
What our shipping terms include
Every order ships with an inspection record that lists the pieces checked, the failures and the action taken. For orders above 100 pieces we photograph the first and last box before sealing.
Minimum order is 50 pieces per design. Stock ships in three to five days and bulk in fifteen to twenty days under 500 pieces, and the inspection runs on the day before dispatch rather than earlier in the week. Payment is a 30 percent deposit with the balance before shipment, by T/T, PayPal or Western Union.
Frequently Asked Questions
Should inspection happen before or after packing?
Before, on the assembled piece, and then a final visual check of the packed box. Inspecting a packed piece means unpacking it again, which reintroduces handling risk.
How do I check plating thickness without a gauge?
You cannot measure it without an instrument. You can compare against a reference piece and you can ask the supplier for a thickness statement. For a programme, buy a coating thickness gauge; it is inexpensive and it settles arguments.
What is the most common defect in a first order?
Uneven plating and short prongs, in roughly equal measure. Both are visible in a two-minute check and both are caught by steps two and four.
Can I inspect remotely?
Partly. Ask for photographs of the first and last box and a copy of the inspection record. Remote inspection works for colour and paperwork, and it does not work for stone seating, which needs a hand.
Next step
Ask for the inspection record with your next order and compare it with what arrives. Our production desk supplies the record as standard, and the guide index covers plating and care decisions.


